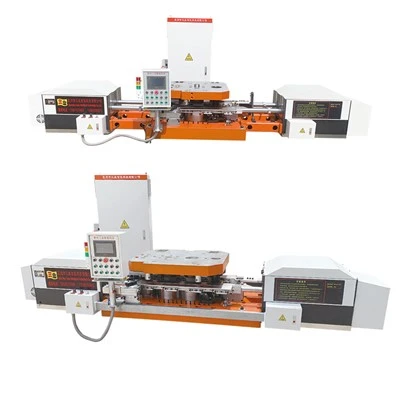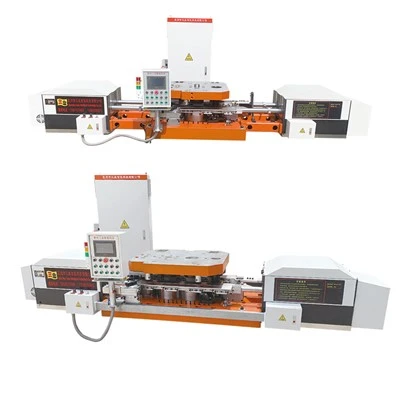


The Nut Bolt Hot Former Machine is an industrial forging machine used to form heated steel billets into nuts and bolts. It performs controlled forming operations through multiple stations for continuous fastener production.


Technical Specifications
|
Specification |
160K-3 |
160K-3G |
200K-3 |
200K-3G |
250K-3 |
250K-3G |
315K-3 |
315K-3G |
400K-3 |
400K-3G |
|
Maximum Clamping Diameter (mm) |
55 |
55 |
60 |
60 |
70 |
70 |
85 |
85 |
100 |
100 |
|
Maximum Clamping Height (mm) |
50 |
50 |
60 |
60 |
60 |
60 |
75 |
75 |
80 |
80 |
|
Production Speed (pcs/min) |
35–45 |
35–45 |
30–40 |
30–40 |
25–35 |
25–35 |
20–30 |
20–30 |
20–30 |
20–30 |
|
Height Adjustment Range (mm) |
0–20 |
0–20 |
0–20 |
0–20 |
0–20 |
0–20 |
0–20 |
0–20 |
0–20 |
0–20 |
|
Crossbeam Lift During Operation (mm) |
- |
0–120 |
- |
0–120 |
- |
0–120 |
- |
0–120 |
- |
0–120 |
|
Stroke (mm) |
170 |
170 |
220 |
220 |
250 |
250 |
250 |
250 |
300 |
300 |
|
Table Dimensions L×W×H (mm) |
700 ×660 ×60 |
700 ×660 ×60 |
800 ×700 ×80 |
800 ×700 ×80 |
800 ×750 ×90 |
800 ×750 ×90 |
800 ×750 ×100 |
800 ×750 ×100 |
1000 ×750 ×110 |
1000 ×750 ×110 |
|
Lower Table Dimensions L×W×H (mm) |
1300 ×760 ×120 |
1300 ×760 ×120 |
1400 ×750 ×130 |
1400 ×750 ×130 |
1500 ×800 ×140 |
1500 ×800 ×140 |
1500 ×800 ×150 |
1500 ×800 ×150 |
1600 ×900 ×160 |
1600 ×900 ×160 |
|
Servo Motor Power (kW) |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
4.5 |
4.5 |
|
Manipulator Overall Dimensions L×W×H (mm) |
3300 ×800 ×700 |
3300 ×800 ×700 |
3400 ×800 ×700 |
3400 ×800 ×700 |
3700 ×1000 ×800 |
3700 ×1000 ×800 |
3600 ×1000 ×800 |
3600 ×1000 ×800 |
4200 ×1200 ×1000 |
4200 ×1200 ×1000 |
|
Manipulator Weight (kg) |
2000 |
2100 |
2500 |
2600 |
2900 |
3000 |
3200 |
3300 |
3700 |
3700 |
Hot Forging Process
Material Feeding: Servo-driven pinch-roll feed system typically meters bar stock with length tolerances within ±0.5 mm to help minimize flash waste.
Induction Heating: Multi-stage medium-frequency furnace generally heats billets up to 1150°C, supported by closed-loop pyrometer control and scale removal options.
Hot Forging: Heavy-duty press is designed for multi-station operations (such as upsetting, extrusion, and piercing) with a rigid frame to help reduce structural deflection.
Automatic Transfer: Multi-axis servo manipulator can be electronically synchronized with the press crank angle to facilitate smooth workpiece transfer.
Forming & Ejection: Progressively shapes components toward net-shape geometries utilizing mechanical ejection mechanisms to route parts to discharge conveyors.
Machine Configuration
Feeding System
Servo-driven hardened rollers handling bar stock up to 100mm with pneumatic clamping.
Induction Heating Furnace
Solid-state IGBT inverters with quick-disconnect cooling and dual infrared sensors for thermal monitoring.
Forging Press
Stress-relieved steel frame with centralized lubrication and pneumatic clutch-brake assemblies.
Automatic Manipulator
Alloy gripper arms with independent servo axes, programmable travel, and torque limits.
Die & Tooling System
Hot-work tool steel (e.g., H13) inserts with thermal coatings and quick-change cassettes.
Control System
Industrial PLC with a touchscreen HMI, safety interlocks, error diagnostics, and recipe storage.
Applications
Nuts
Hex nuts, heavy hex nuts, flange nuts, lock nuts and other forged nut blanks.
Bolts & Fasteners
Hot-formed bolt heads and other large-size or high-volume fastener components.
Washers
Hot-forged washers and ring-shaped parts requiring upsetting and piercing.
Bearing Rings
Ring blanks produced by hot upsetting and piercing operations.
Special Forged Parts
Custom-shaped components according to product drawing, material and forging requirements.


Customization
Plant Layout & Infrastructure: Tailor equipment footprints, load distribution (2000kg–3700kg), input voltages, and cooling interfaces to your facility.
Tooling, Stroke & Clamping: Modify clamping diameters (55mm–100mm), heights (50mm–80mm), strokes (170mm–300mm), and table dimensions for non-standard fasteners.
Material & Thermal Parameters: Configure induction heating frequencies and thermal curves for high-alloy or stainless steel up to 1000°C.
Engineering Workflow: Submit drawings and constraints for direct senior engineering review, specification sign-off, and custom manufacturing.
Quality Testing
Raw Material Verification: Ultrasonic and metallurgical testing of incoming high-alloy stock to ensure material integrity prior to thermal processing.
Thermal & Sensor Calibration: Rigorous thermal profiling of induction heating zones (up to 1000°C) and calibration of closed-loop servo sensors to maintain precise temperature and speed regulation.
Dimensional & Tolerance Inspection: Post-forging verification of clamping dimensions, stroke accuracy, and structural geometry against international fastener standards.
Full-Line Factory Run-off: Comprehensive load testing and synchronization trials of the integrated feeder, furnace, press, and manipulator prior to shipment.
Installation & After-Sales
On-Site Commissioning: Factory-certified engineers provide direct on-site installation, machine leveling, and initial operational calibration.
Technical Training: Comprehensive on-site training for your operators and maintenance team covering PLC programming, routine maintenance, and safety protocols.
Remote Diagnostic Assistance: Dedicated technical support team available for remote troubleshooting, operational guidance, and firmware updates.
Spare Parts Availability: Dedicated inventory channels ensuring rapid dispatch of replacement mechanical and electrical components to minimize downtime.
FAQ
Q: What utilities are required for operation?
A: Stable 3-phase industrial power for the servo motors and induction furnace, plus an industrial water-cooling supply.
Q: How is technical training handled for our operators?
A: Factory engineers provide on-site training covering routine maintenance, sensor calibration, and PLC troubleshooting.
Q: Are spare parts kept in stock?
A: Yes, critical wear parts and standard components are stocked for rapid international dispatch.
Q: What foundation preparation is needed?
A: A reinforced concrete foundation designed to support the combined dynamic load of the press and the 2000kg–3700kg manipulator.
Q: Can the line process different material grades?
A: Yes, heating profiles and control systems are adjustable for alloy steels, stainless steel, and specialized fastener materials.
Q: How is the equipment packaged for export?
A: Modular components are packed in heavy-duty, moisture-sealed export-grade wooden crates for containerized freight.
Hot Tags: nut bolt hot former machine, China nut bolt hot former machine manufacturers, suppliers, factory, hot forging Slotted nut bolt, hot pressing lock nut bolt, hot stamping castel nut bolt, hot stamping lock nut bolt, Nut Bolt Former Automatic Machine, Nut Bolt Former Machine