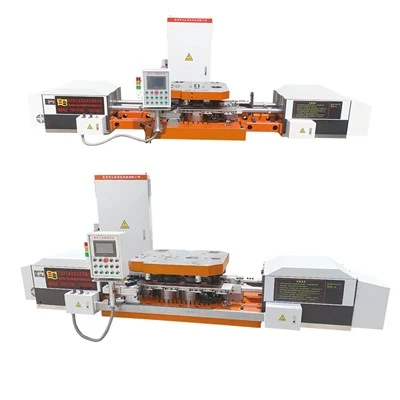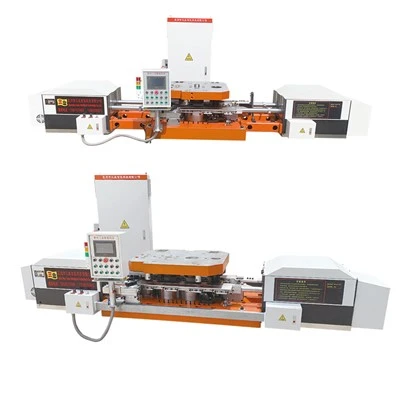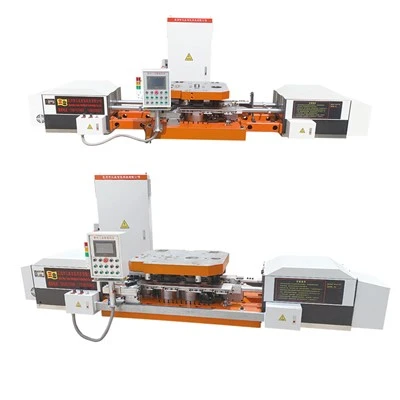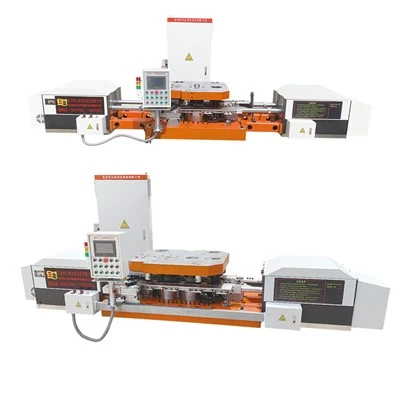


The Nut Former Automatic Manipulator is a heavy-duty, multi-station automation unit engineered to convert manual or semi-automatic hot forging presses into high-speed nut production lines.


Product Specification
|
MODEL |
160K-3 |
160K-3G |
200K-3 |
200K-3G |
250K-3 |
250K-3G |
315K-3 |
315K-3G |
400K-3 |
400K-3G |
|
MAX CLAMP DIAMETER(mm) |
55 |
55 |
60 |
60 |
70 |
70 |
85 |
85 |
100 |
100 |
|
MAX CLAMP HEIGHT(mm) |
50 |
50 |
60 |
60 |
60 |
60 |
75 |
75 |
80 |
80 |
|
SPEED(PCS/min) |
35-45 |
35-45 |
30-40 |
30-40 |
25-35 |
25-35 |
20-30 |
20-30 |
20-30 |
20-30 |
|
HEIGHT ADJUSTING RANGE(mm) |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
|
BEAM LIFTING HEIGHT DURING WORKING |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
|
STROKE(mm) |
170 |
170 |
220 |
220 |
250 |
250 |
250 |
250 |
300 |
300 |
|
TOP TABLE DIMENSION(mm)L*W*H |
700 * 660 * 60 |
700 * 660 * 60 |
800 * 700 * 80 |
800 * 700 * 80 |
800 * 750 * 90 |
800 * 750 * 90 |
800 * 750 * 100 |
800 * 750 * 100 |
1000 * 750 * 110 |
1000 * 750 * 110 |
|
DOWN TABLE DIMENSION (mm)L*W*H |
1300 * 760 * 120 |
1300 * 760 * 120 |
1400 * 750 * 130 |
1400 * 750 * 130 |
1500 * 800 * 140 |
1500 * 800 * 140 |
1500 * 800 * 150 |
1500 * 800 * 150 |
1600 * 900 * 160 |
1600 * 900 * 160 |
|
SERVO MOTOR POWER(KW) |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
4.5 |
4.5 |
|
MANUPULATOR OVERALL DIMENSION(MM)L*W*H |
3300 * 800 * 700 |
3300 * 800 * 700 |
3400 * 800 * 700 |
3400 * 800 * 700 |
3700 * 1000 * 800 |
3700 * 1000 * 800 |
3600 * 1000 * 800 |
3600 * 1000 * 800 |
4200 * 1200 * 100 |
4200 * 1200 * 100 |
|
MANIPULATOR WEIGHT(Kg) |
2000 |
2100 |
2500 |
2600 |
2900 |
3000 |
3200 |
3300 |
3700 |
3700 |
Nut Types
Standard Hex Nuts: Forging of M12–M36 metric and imperial hex nuts conforming to DIN 934, ISO 4032, and ASME B18.2.2 specifications.
Flange & Automotive Nuts: Forming of integral flange, wheel, and locknut blanks for automotive chassis, suspension, and axle assemblies.
Heavy-Duty Structural Locknuts: Processing of Grade 8.8, 10.9, and 12.9 alloy steel raw stock into thick-walled fasteners for mining, structural steel, and railways.
Custom Forged Components: Multi-station forming of non-standard, asymmetric, and stepped industrial hardware engineered to customer engineering drawings.
Hot Forging Process
Induction Heating & Feeding: Mid-frequency induction units maintain the billet temperature within ±15°C before it is mechanically transferred to the first die.
Multi-Station Upsetting: Progressive pre-forming and body-forming dies redistribute the raw stock volume to prevent surface folds and material cracking.
Piercing & Chamfering: An integrated mechanical punch station creates clean center bores and outer-edge chamfers in a single press stroke.
Automated Station Transfer: Cam-driven transfer fingers move workpieces between dies at throughput speeds of up to 120 pieces per minute.


Installation Requirements
Foundation: Concrete pad with damping mounts designed to isolate operational kinetic impacts from surrounding plant infrastructure.
Electrical Supply: 380V/415V, 50/60Hz, 3-phase connection with built-in voltage stabilization for the induction heater.
Pneumatic & Cooling Utilities: Operational line pressure of 0.6–0.8 MPa compressed air paired with a closed-loop water system delivering a constant 15–20°C flow.
Lubrication & Scale Flushing: Centralized automatic oil lubrication coupled with high-pressure fluid channels under the bed.
Delivery & After-Sales Support
Factory Acceptance Test (FAT): Includes a continuous 100-piece production run using customer-specified steel grades and CAD drawings before packing.
On-Site Commissioning: Field technician deployment for foundation leveling, tooling alignment, electrical integration, and operator machine training.
Consumable & Wear Parts Stock: Standard punches, dies, and transfer fingers maintained in regional hubs for dispatch.
Warranty: 12-month structural warranty covering the main crankshaft and flywheel assembly, backed by Ethernet PLC remote diagnostics.
FAQ
Q: What nut size range achieves the maximum 120 pieces per minute?
A: The 120 PPM peak throughput is achieved on smaller M12-M20 standard hex nuts; larger flange nuts and heavy-duty locknuts above M24 typically run at 70-90 PPM due to increased material mass per stroke.
Q: What happens to the crankshaft and flywheel warranty if the equipment is used beyond standard three-shift operation?
A: The 12-month structural warranty remains valid under standard three-shift usage; continuous 24/7 operation beyond this profile requires prior notification to maintain full warranty coverage.
Q: Can we specify our own steel grade and design drawings for the Factory Acceptance Test?
A: Yes, the FAT includes a continuous 100-piece production run using your specified steel grade and CAD drawings, ensuring the equipment is ready before shipment.
Q: What voltage and utility conditions must our facility meet?
A: Your facility needs a 380V/415V 50/60Hz three-phase electrical supply, 0.6-0.8 MPa compressed air, and a closed-loop water cooling system maintaining 15-20°C flow.
Q: What information is required to select the correct nut former equipment?
A: The key selection data includes nut dimensions, blank weight, forging material, required production rate, press capacity, number of forging stations, and existing press configuration.
Hot Tags: nut former automatic machine, China nut former automatic machine manufacturers, suppliers, factory, hot forming lock nut, hot pressing flange nut, hot pressing wheel nut line, hot stamping Slotted nut, Nut Former Automatic Machine Line, Nut Hot Former Automatic Machine