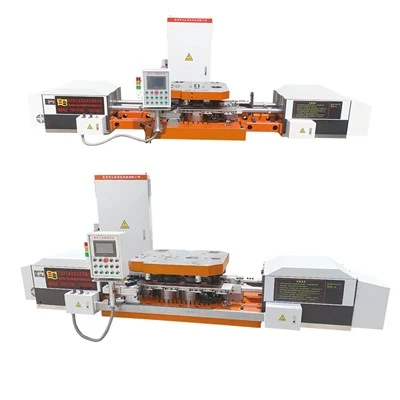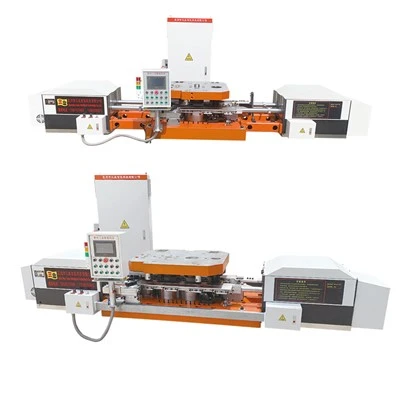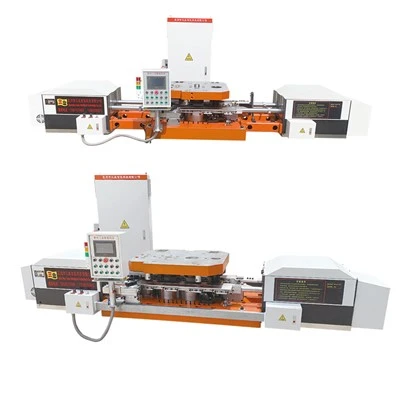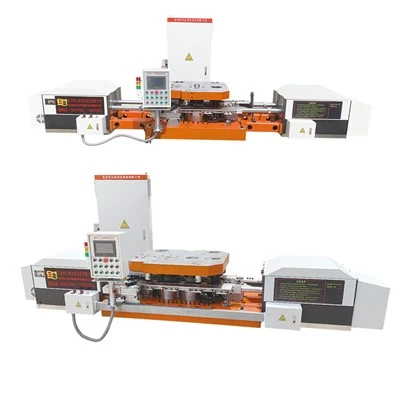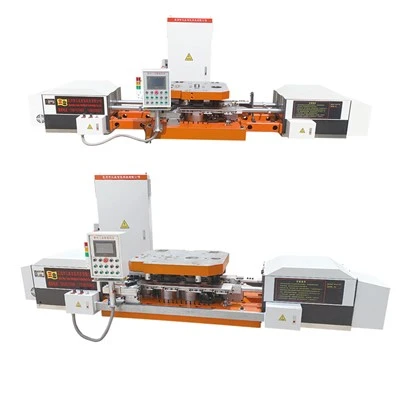


The Nut Former Machine Line feeds, grips, and transfers heated metal slugs through sequential forming dies to manufacture heavy-duty industrial nuts and axisymmetric hardware components.


Product Specification
|
MODEL |
160K-3 |
160K-3G |
200K-3 |
200K-3G |
250K-3 |
250K-3G |
315K-3 |
315K-3G |
400K-3 |
400K-3G |
|
MAX CLAMP DIAMETER(mm) |
55 |
55 |
60 |
60 |
70 |
70 |
85 |
85 |
100 |
100 |
|
MAX CLAMP HEIGHT(mm) |
50 |
50 |
60 |
60 |
60 |
60 |
75 |
75 |
80 |
80 |
|
SPEED(PCS/min) |
35-45 |
35-45 |
30-40 |
30-40 |
25-35 |
25-35 |
20-30 |
20-30 |
20-30 |
20-30 |
|
HEIGHT ADJUSTING RANGE(mm) |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
|
BEAM LIFTING HEIGHT DURING WORKING |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
|
STROKE(mm) |
170 |
170 |
220 |
220 |
250 |
250 |
250 |
250 |
300 |
300 |
|
TOP TABLE DIMENSION(mm)L*W*H |
700 * 660 * 60 |
700 * 660 * 60 |
800 * 700 * 80 |
800 * 700 * 80 |
800 * 750 * 90 |
800 * 750 * 90 |
800 * 750 * 100 |
800 * 750 * 100 |
1000 * 750 * 110 |
1000 * 750 * 110 |
|
DOWN TABLE DIMENSION (mm)L*W*H |
1300 * 760 * 120 |
1300 * 760 * 120 |
1400 * 750 * 130 |
1400 * 750 * 130 |
1500 * 800 * 140 |
1500 * 800 * 140 |
1500 * 800 * 150 |
1500 * 800 * 150 |
1600 * 900 * 160 |
1600 * 900 * 160 |
|
SERVO MOTOR POWER(KW) |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
4.5 |
4.5 |
|
MANUPULATOR OVERALL DIMENSION(MM)L*W*H |
3300 * 800 * 700 |
3300 * 800 * 700 |
3400 * 800 * 700 |
3400 * 800 * 700 |
3700 * 1000 * 800 |
3700 * 1000 * 800 |
3600 * 1000 * 800 |
3600 * 1000 * 800 |
4200 * 1200 * 100 |
4200 * 1200 * 100 |
|
MANIPULATOR WEIGHT(Kg) |
2000 |
2100 |
2500 |
2600 |
2900 |
3000 |
3200 |
3300 |
3700 |
3700 |
Forging Force & Machine Performance
Forging Capacity: Delivers 35–45 strokes/min on 160-ton models and 20–30 strokes/min on heavy-duty 400-ton lines.
Thermal Protection: Water-cooled grippers and thermal barriers protect pneumatic and electronic sensors in forging environments exceeding 1000°C.
Continuous Stability: The heavy-duty cast-iron body dampens vibrations from continuous forging, maintaining precise alignment under maximum load.
Multi-Station Forming Configuration
Multi-Stage Transfers: Configurable for 3-station and 4-station sequences: Descaling/Upsetting → Forming/Hexing → Piercing/Punching.
Dynamic Clearance: Motorized beam lift ("G" series) offers 0–120 mm clearance for complex lower dies and raised ejector pins.
Tooling Stroke: Integrated 0–20 mm bolster adjustment accommodates thick custom die blocks without shimming.
Quick-Release Grippers: Mechanical quick-change gripper arms enable complete die set changes in under 30 minutes.


Customization Options
Geometry Tailoring: Custom station layouts engineered for specific cross-flat dimensions, flange diameters, and non-standard nut profiles.
Material: Machine power and induction heating systems configured for specific alloy grades, stainless steels, and billet sizes.
Process Flow Sequence: Custom station mapping for unique combinations of upsetting, piercing, expanding, and sizing.
Plant & Automation Integration: Customized machine footprint, material feed direction, utility connections, auto-feeders, billet elevators, and robotic bin-picking systems.
Quality Control
Transfer Repeatability: Servo-driven transfers hold multi-station positioning tolerances within ±0.15 mm across all passes.
Die Protection Interlocks: Thermal sensors and double-blank detectors stop the press instantly upon misfeed to prevent die crashes.
Standard Compliance: Maintains wall thickness and concentricity to meet ISO 4759-1 and DIN 934 fastener specifications.
In-Line Force Monitoring: Real-time tonnage sensors track forging load per station to detect worn tooling before defects occur.
Delivery Terms
Lead Time: Standard configurations ship in 80–120 calendar days following a mandatory 72-hour pre-shipment dry run.
Tooling Package: Includes Cr-Mo-V alloy initial dies and a 12-month wearable spares kit (grippers, punches, push rods).
Export Packaging: Sealed in VCI anti-rust film and packed in sea-worthy steel-framed wooden crates with full CE/ISO compliance files.
Commissioning & Support: Covers 10 days of on-site installation and operator training, backed by a 48-hour global field service response.
FAQ
Q: What warranty period applies to the main press frame and servo transfer system, separate from the wearable spares kit?
A: The main press body and servo-driven transfer system carry a 24-month structural warranty, distinct from the 12-month wearable spares package already included.
Q: What is the typical service life of the cast-iron press body before major overhaul is needed?
A: Under normal three-shift operation, the cast-iron body and main bearings typically run 12-15 years before requiring a major structural overhaul.
Q: Do you offer factory acceptance testing (FAT) before shipment?
A: Yes, we conduct FAT with live video streaming for overseas buyers who cannot travel, in addition to the standard 72-hour pre-shipment dry run already performed on-site.
Q: What payment terms are typically offered for a full nut former line?
A: Standard terms are 30% deposit, 60% before shipment, and 10% after commissioning acceptance, with T/T or L/C accepted.
Q: What is the average electricity consumption for a 400-ton heavy-duty line during full production?
A: A 400-ton configuration typically draws 75-90 kW/h under continuous multi-station operation, depending on billet size and stroke rate.
Hot Tags: nut former machine line, China nut former machine line manufacturers, suppliers, factory, hot forging Slotted nut, hot forming square nut, hot making acorn nut, hot making castel nut, hot making Slotted nut, hot pressing lock nut