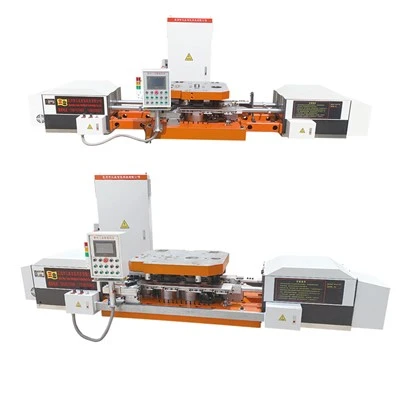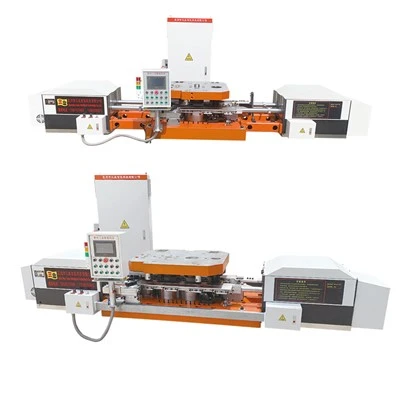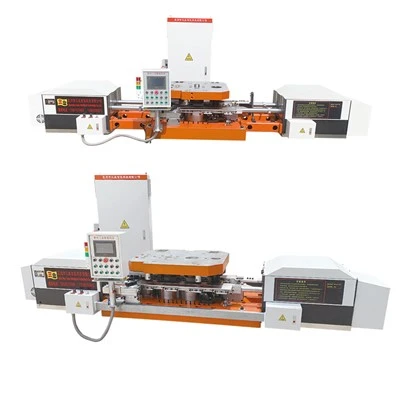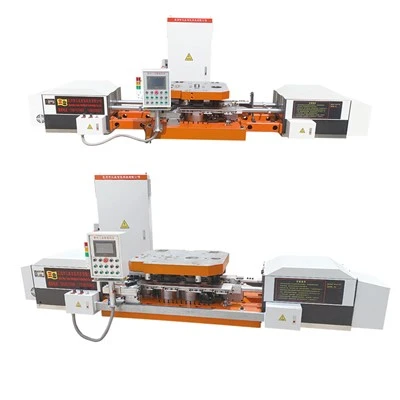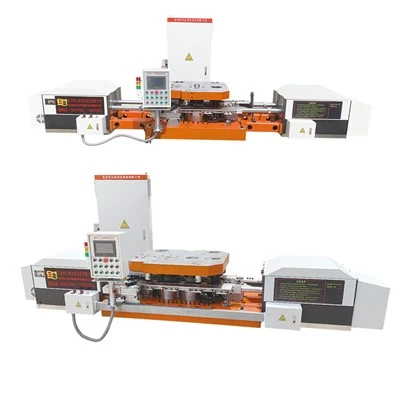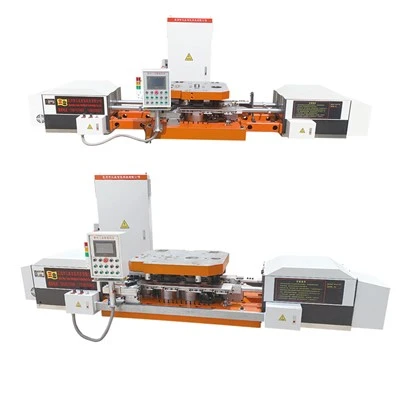

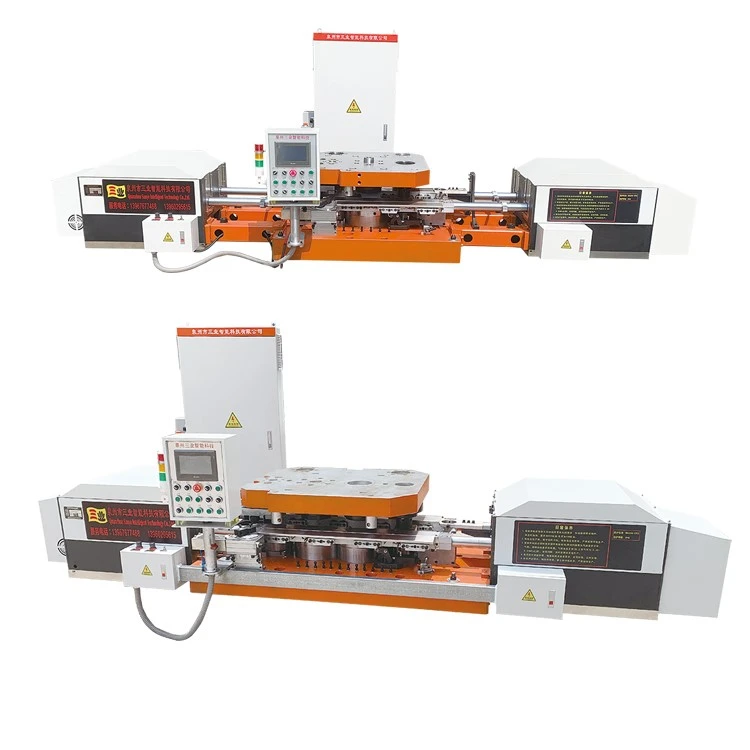
A nut former manipulator is an automated transfer unit for C-frame and gantry hot forging presses. It moves heated blanks through sequential dies to produce hex nuts, bearing rings, and heavy-duty automotive fasteners.


Product Specification
|
MODEL |
160K-3 |
160K-3G |
200K-3 |
200K-3G |
250K-3 |
250K-3G |
315K-3 |
315K-3G |
400K-3 |
400K-3G |
|
MAX CLAMP DIAMETER (mm) |
55 |
55 |
60 |
60 |
70 |
70 |
85 |
85 |
100 |
100 |
|
MAX CLAMP HEIGHT (mm) |
50 |
50 |
60 |
60 |
60 |
60 |
75 |
75 |
80 |
80 |
|
SPEED (PCS/min) |
35-45 |
35-45 |
30-40 |
30-40 |
25-35 |
25-35 |
20-30 |
20-30 |
20-30 |
20-30 |
|
HEIGHT ADJUSTING RANGE (mm) |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
|
BEAM LIFTING HEIGHT DURING WORKING |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
|
STROKE (mm) |
170 |
170 |
220 |
220 |
250 |
250 |
250 |
250 |
300 |
300 |
|
TOP TABLE DIMENSION (mm) L*W*H |
700 * 660 * 60 |
700 * 660 * 60 |
800 * 700 * 80 |
800 * 700 * 80 |
800 * 750 * 90 |
800 * 750 * 90 |
800 * 750 * 100 |
800 * 750 * 100 |
1000 * 750 * 110 |
1000 * 750 * 110 |
|
DOWN TABLE DIMENSION (mm) L*W*H |
1300 * 760 * 120 |
1300 * 760 * 120 |
1400 * 750 * 130 |
1400 * 750 * 130 |
1500 * 800 * 140 |
1500 * 800 * 140 |
1500 * 800 * 150 |
1500 * 800 * 150 |
1600 * 900 * 160 |
1600 * 900 * 160 |
|
SERVO MOTOR POWER (KW) |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
4.5 |
4.5 |
|
MANUPULATOR OVERALL DIMENSION (MM) L*W*H |
3300 * 800 * 700 |
3300 * 800 * 700 |
3400 * 800 * 700 |
3400 * 800 * 700 |
3700 * 1000 * 800 |
3700 * 1000 * 800 |
3600 * 1000 * 800 |
3600 * 1000 * 800 |
4200 * 1200 * 100 |
4200 * 1200 * 100 |
|
MANIPULATOR WEIGHT (Kg) |
2000 |
2100 |
2500 |
2600 |
2900 |
3000 |
3200 |
3300 |
3700 |
3700 |
Typical Applications
Standard Industrial Hex Nuts: Forges M16–M48 heavy hex nuts designed for structural steel, power grids, and infrastructure.
Automotive Fasteners: Produces high-grade wheel nuts, lug nuts, and Class 8.8–12.9 suspension nut blanks.
Bearing Ring Blanks: Performs multi-station hot forging for inner/outer bearing rings up to 100 mm OD, eliminating thermal scarring.
Pipe Couplings & Lock Nuts: Forges high-pressure oil/gas pipe couplings, hydraulic union nuts, and serrated lock nuts.
Material Compatibility
Carbon Steel Alloys
Processes AISI 1020, 1045, and 1050 steel billets preheated to 1,000°C–1,200°C.
High-Tensile Alloy Steels
Forges 40Cr, 42CrMo, and 20CrMnTi alloys engineered for high-stress industrial applications.
Stainless Steel Grades
Accommodates SUS 304, 316, and 410 stainless steel billets under precise clamping pressure.


Working Principle
Induction Infeed & Clamping: Pre-heated billets from the furnace pass directly into high-speed pneumatic grippers.
Servo Progression & Lift: Dual-axis servo drives advance workpieces across stations 1–3 with a 120 mm vertical lift.
TDC Synchronized Retraction: Optical encoders monitor press angle, triggering gripper retraction 5° before Top Dead Center impact.
Part Discharge: Finished forging blanks drop into the discharge chute within a continuous 1.2-second cycle time.
Production Control
Industrial Protocol Integration: PLC controller supports native Modbus TCP and EtherNet/IP for direct integration into plant MES networks.
Multilingual HMI: 10-inch touchscreen (English, German, Spanish, Turkish) stores up to 50 operational parameter profiles for fast setup.
Real-Time Diagnostics: Continuous monitoring of line pressure, die temperature, and axis timing alerts operators before bad parts are forged.
Manufacturing Capabilities
Direct Manufacturer: Built by Quanzhou Sanye Intelligent Technology Co., Ltd. (Fujian, China), specializing in automated hot forging machinery.
Patented R&D: Holds State High-Tech Enterprise status with proprietary patents in multi-axis transfer systems and thermal gripper mechanics.
Factory Testing: Every machine completes a 72-hour full-load dry run before seaworthy export packaging.
FAQ
Q: Which export markets does the multilingual HMI (English, German, Spanish, Turkish) primarily support?
A: These language options directly serve our active customer base in the United States, Argentina, Türkiye, and other Spanish- and German-speaking industrial markets.
Q: What nut or bearing ring size range achieves the 1.2-second continuous cycle time?
A: The 1.2-second cycle time applies to M16-M30 hex nuts and bearing rings up to 80mm OD; larger M36-M48 heavy hex nuts typically run at 1.8-2.2 second cycles due to increased material transfer mass.
Q: What warranty coverage applies to the servo drives and gripper mechanics?
A: The servo drive system and gripper mechanics carry a 12-month warranty covering manufacturing defects, separate from consumable wear parts like grippers and transfer fingers.
Q: What is the standard lead time from order confirmation to completion of factory testing?
A: The standard lead time from order confirmation to completion of the 72-hour dry run and export packaging is 85-100 calendar days for standard configurations.
Q: What payment terms and methods are accepted for international orders?
A: We accept T/T and L/C payment methods, with standard terms of 30% deposit upon order confirmation and 70% balance before shipment after the customer approves FAT results.
Hot Tags: nut former machine, China nut former machine manufacturers, suppliers, factory, hot forming castel nut, hot making square nut, hot punching Slotted nut, hot stamping castel nut, Nut Former Automatic Equipment, Nut Hot Former Machine