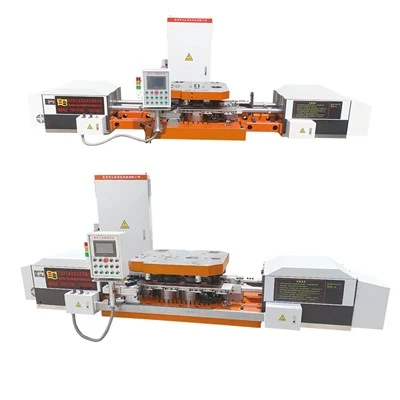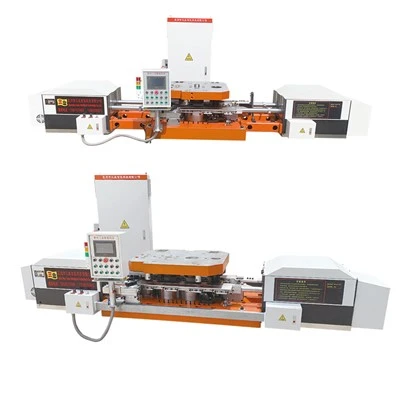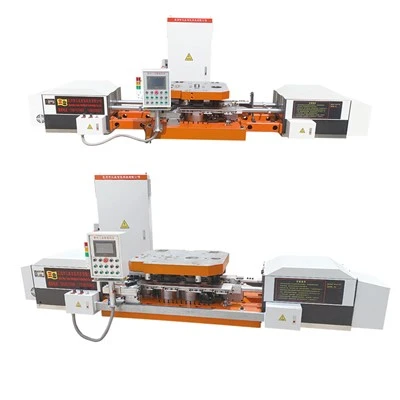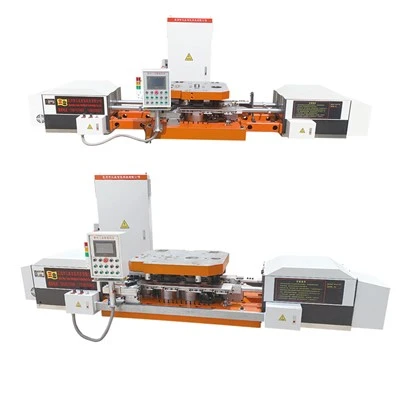


A Nut Former Automatic Equipment (Hot Forging Manipulator) is a motorized robotic transfer system designed to automate workpiece feeding, repositioning, and ejection across multiple hot forging die stations.


Product Specification
|
MODEL |
160K-3 |
160K-3G |
200K-3 |
200K-3G |
250K-3 |
250K-3G |
315K-3 |
315K-3G |
400K-3 |
400K-3G |
|
MAX CLAMP DIAMETER(mm) |
55 |
55 |
60 |
60 |
70 |
70 |
85 |
85 |
100 |
100 |
|
MAX CLAMP HEIGHT(mm) |
50 |
50 |
60 |
60 |
60 |
60 |
75 |
75 |
80 |
80 |
|
SPEED(PCS/min) |
35-45 |
35-45 |
30-40 |
30-40 |
25-35 |
25-35 |
20-30 |
20-30 |
20-30 |
20-30 |
|
HEIGHT ADJUSTING RANGE(mm) |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
0-20 |
|
BEAM LIFTING HEIGHT DURING WORKING |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
/ |
0-120 |
|
STROKE(mm) |
170 |
170 |
220 |
220 |
250 |
250 |
250 |
250 |
300 |
300 |
|
TOP TABLE DIMENSION(mm)L*W*H |
700 * 660 * 60 |
700 * 660 * 60 |
800 * 700 * 80 |
800 * 700 * 80 |
800 * 750 * 90 |
800 * 750 * 90 |
800 * 750 * 100 |
800 * 750 * 100 |
1000 * 750 * 110 |
1000 * 750 * 110 |
|
DOWN TABLE DIMENSION (mm)L*W*H |
1300 * 760 * 120 |
1300 * 760 * 120 |
1400 * 750 * 130 |
1400 * 750 * 130 |
1500 * 800 * 140 |
1500 * 800 * 140 |
1500 * 800 * 150 |
1500 * 800 * 150 |
1600 * 900 * 160 |
1600 * 900 * 160 |
|
SERVO MOTOR POWER(KW) |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
3 |
4.5 |
4.5 |
4.5 |
|
MANUPULATOR OVERALL DIMENSION(MM)L*W*H |
3300 * 800 * 700 |
3300 * 800 * 700 |
3400 * 800 * 700 |
3400 * 800 * 700 |
3700 * 1000 * 800 |
3700 * 1000 * 800 |
3600 * 1000 * 800 |
3600 * 1000 * 800 |
4200 * 1200 * 100 |
4200 * 1200 * 100 |
|
MANIPULATOR WEIGHT(Kg) |
2000 |
2100 |
2500 |
2600 |
2900 |
3000 |
3200 |
3300 |
3700 |
3700 |
Nut Types & Applications
M18–M48 hex flange nuts (Grades 8.8, 10.9, 12.9) for commercial vehicle wheel hubs and axle systems.
Heavy hex nuts and structural sleeve anchors engineered for civil engineering projects.
Stainless steel and nickel-alloy locknuts designed for high-pressure, corrosive pipeline environments.
Thick-walled square nuts, weld nuts, and custom collar fasteners built for heavy farm equipment.
Nut Forging Line Construction
Induction Heating & Optical Inspection: Synchronized billet feeding maintains a strict ±15°C forging temperature window, while the thermal sorting system automatically rejects underheated billets.
Timed Die Lubrication: Programmable graphite spray nozzles maximize die life and reduce consumable costs.
Automated Discharge System: Motorized cooling conveyors route hot parts directly to tapping operations.
Siemens PLC System: Pre-configured recipe management stores 50 part profiles for rapid job setup.
Modular Tooling: Standardized clamp assemblies enable complete multi-station die changes in under 20 minutes.


Performance Verification
1000°C Thermal Load Run: Continuous full-load thermal stress testing verifying cooling and drive stability before dispatch.
Laser Alignment Calibration: Transfer mechanism repeatability verified using laser trackers within ±0.08 mm precision.
Customer Tooling Validation: Pre-shipment trial production using buyer-supplied dies to guarantee target dimensions and output rates.
FAT Audit Documentation: Comprehensive FAT package provided, including signed safety logs, noise test reports (<78 dB), and electrical inspection certificates.
Safety Systems & CE Compliance
Dual-Circuit Safety Interlock: Hardwired E-stop triggering mechanical braking within 80 ms during operational anomalies.
Perimeter Guarding: Category 4 / SIL 3 optical light curtains instantly halting machinery upon barrier breach.
Mechanical Overload Protection: Real-time torque monitoring halting press stroke instantly to prevent double-billet die damage.
Global Safety Certification: Built fully compliant with European CE (2006/42/EC) and North American ANSI/B11 standards.
Engineering Support
On-Site Turnkey Commissioning
Field service engineers dispatched globally for line integration, setup, and operator training.
Express Spare Parts Dispatch
Critical wear parts, grippers, and seal kits stocked for global shipment within 24–48 hours.
Remote Diagnostic Support
Direct PLC network connection for real-time troubleshooting to minimize operational downtime.
FAQ
Q: How does your ±0.08 mm laser-verified repeatability compare to typical manipulators in this industry?
A: Most hot forging manipulators on the market operate within ±0.15-0.2 mm repeatability, so our laser-tracker-verified ±0.08 mm precision roughly doubles typical positioning accuracy for critical nut and bearing ring geometries.
Q: Can we request copies of your CE and ANSI/B11 certification documents before placing an order?
A: Yes, we provide certification documents including certificate numbers and issuing body details as part of the pre-order technical package upon request.
Q: How is the 80 ms emergency stop response time verified during testing?
A: The 80 ms mechanical braking response is measured and logged during the pre-shipment FAT using calibrated timing sensors, with results included in the signed safety log.
Q: Can customers send their own dies for trial production before finalizing the purchase?
A: Yes, our Customer Tooling Validation process allows buyers to ship their own dies for a pre-shipment trial run, confirming target dimensions and output rates before the equipment leaves our factory.
Q: What is the standard lead time from order confirmation to shipment for this equipment line?
A: Standard lead time is 90-110 calendar days, which includes the 1000°C thermal load run and full FAT documentation process prior to dispatch.
Hot Tags: nut former automatic equipment, China nut former automatic equipment manufacturers, suppliers, factory